Moisture Sensor Commissioning Checklist Cement Kiln Clinker Cooler
Moisture Sensor Commissioning Checklist Cement Kiln Clinker Cooler
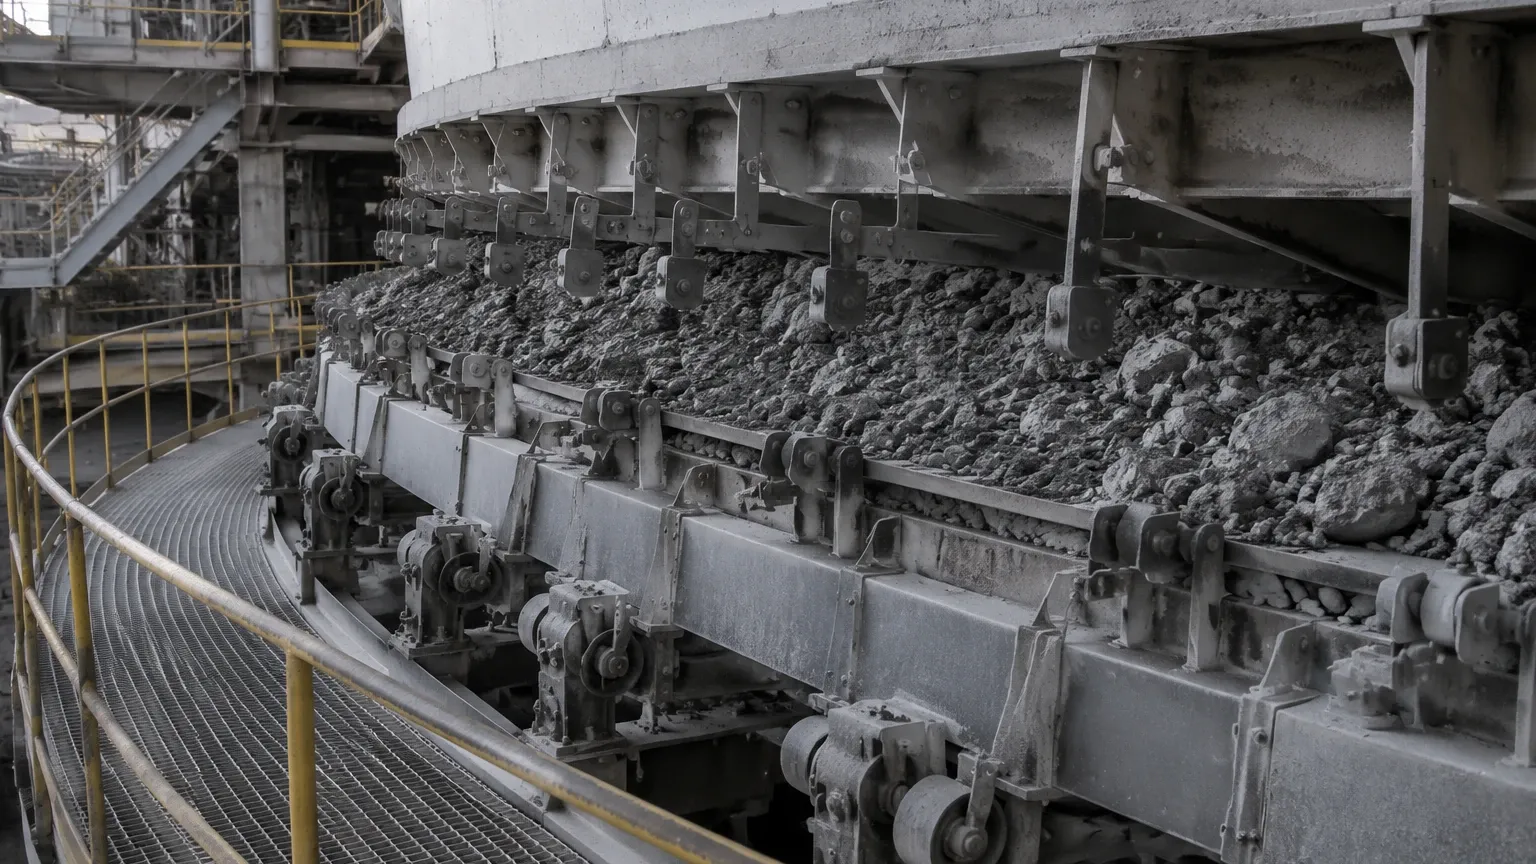
In the production of cement, the clinker cooler serves a vital role in thermal efficiency and product quality. As the clinker exits the rotary kiln at temperatures exceeding 1,400°C, it must be rapidly cooled to approximately 100°C to 200°C before being transported to storage or the grinding mill. Moisture control during this stage—often involving water spray systems for cooling—is critical. Excessive moisture can lead to clinker hydration, clogging of transport systems, and reduced efficiency in the ball mills, while insufficient moisture may result in inadequate cooling.
Implementing a robust moisture sensor commissioning checklist cement kiln clinker cooler ensures that the instrumentation provides the accurate, real-time data necessary for automated process control. This guide outlines the technical principles, selection criteria, and a comprehensive commissioning framework for engineering teams.
Measurement Principles for Clinker Moisture
Before initiating a commissioning checklist, it is essential to understand the physics behind the measurement technologies used in the harsh environment of a cement plant. Most moisture sensors for clinker applications utilize either microwave or near-infrared (NIR) technology.
Microwave Moisture Measurement
Microwave sensors operate on the principle of the high dielectric constant of water compared to dry clinker. When microwaves pass through the material, the water molecules rotate in an attempt to align with the high-frequency electromagnetic field. This results in energy loss (attenuation) and a change in the signal's phase. Because microwaves penetrate the material, they provide a representative measurement of the entire volume, not just the surface.
Near-Infrared (NIR) Reflectance
NIR sensors project light at specific wavelengths onto the clinker surface. Water molecules absorb specific bands of infrared light. By measuring the ratio of reflected light at a reference wavelength versus an absorption wavelength, the sensor calculates the surface moisture. While highly accurate for surface readings, NIR can be affected by dust and changes in material color or grain size.
Comparison of Technologies
| Feature | Microwave (Contact/Non-Contact) | Near-Infrared (NIR) |
| :— | :— | :— |
| Measurement Depth | Full volume penetration | Surface only |
| Dust Sensitivity | Low | High (Requires air purging) |
| Temperature Limit | Up to 120°C (Sensor head) | Up to 60°C (Requires cooling) |
| Accuracy | ±0.5% typical | ±0.2% typical |
| Maintenance | Low | Moderate (Lens cleaning) |
Moisture Sensor Commissioning Checklist Cement Kiln Clinker Cooler
A successful commissioning process is divided into four distinct phases: Pre-Installation Verification, Mechanical Installation, Electrical Integration, and Calibration/Validation.
1. Pre-Installation Verification
Before the sensor is mounted on the conveyor or cooler exit, verify the following:
* Specification Match: Confirm the sensor’s measurement range (typically 0–5% moisture for clinker) matches the process requirements.
* Environmental Protection: Ensure the sensor housing is rated for the ambient temperature. In clinker coolers, this often requires a vortex cooler or water-cooling jacket.
* Component Integrity: Inspect the sensor face (microwave window or NIR lens) for scratches or manufacturing defects.
* Documentation: Collate all factory calibration certificates and safety data sheets for the commissioning file.
2. Mechanical Installation Checklist
The physical location of the sensor is the most frequent cause of measurement error. Follow these steps during installation:
* Mounting Location: The sensor should be placed where the material flow is consistent. On a belt conveyor, this is ideally 2 to 3 meters after a transfer point where the material has leveled out.
* Material Height: For microwave sensors, a minimum material bed depth (usually 50 mm to 100 mm) is required to ensure the signal interacts with enough material.
* Vibration Isolation: Ensure the mounting bracket is rigid and isolated from the heavy vibrations of the clinker cooler’s reciprocating grates.
* Cleaning Access: Verify that technicians can safely reach the sensor for routine cleaning without stopping the production line.
* Protection: Install a "plow" or leveling bar upstream of the sensor to maintain a uniform distance between the sensor and the clinker surface.
3. Electrical and Signal Integration
Once mounted, the sensor must be integrated into the plant’s PLC/DCS system:
* Power Supply: Confirm the voltage (typically 24V DC or 110/230V AC) is stable and within the sensor’s tolerance.
* Signal Shielding: Use shielded twisted-pair cabling for 4-20mA or RS485 signals to prevent electromagnetic interference from large kiln motors.
* Grounding: Ensure the sensor and the mounting structure share a common ground to prevent ground loops.
* Output Scaling: Configure the DCS to match the sensor’s output (e.g., 4mA = 0% moisture, 20mA = 5% moisture).
4. Calibration and Sampling (The Critical Step)
No moisture sensor is "plug-and-play" in a cement environment. Field calibration against laboratory standards is mandatory.
* Zero Calibration: Perform a "dry run" with no material on the belt to establish the baseline signal.
* Reference Sampling: Collect at least 5 to 10 samples of clinker directly from the sensor location during operation. Immediately seal these samples in airtight containers.
* Laboratory Analysis: Use the "Loss on Drying" (LOD) method in the plant lab to determine the actual moisture content of the samples.
* Curve Fitting: Input the laboratory values into the sensor’s software to create a calibration curve. Most modern sensors use a linear or polynomial regression model.
* Validation: After applying the calibration, take a new set of samples the following day to verify the sensor’s reading matches the lab results within the specified tolerance (e.g., ±0.5%).
Installation Considerations and Limitations
When following the moisture sensor commissioning checklist cement kiln clinker cooler, engineers must account for several site-specific variables that can impact performance.
Temperature Extremes
Clinker exiting the cooler can still be hot enough to damage standard electronics. If the material temperature exceeds 100°C, non-contact microwave sensors or NIR sensors with high-temperature optics are required. If using contact-based sensors (like ceramic-faced microwave probes), ensure the mounting can withstand thermal expansion of the chute or conveyor frame.
Dust and Build-up
The cement industry is inherently dusty. For NIR sensors, an air purge system is essential to keep the optical window clear. For microwave sensors, while dust is less of an issue, a thick crust of hardened clinker dust on the sensor face can cause signal drift. Regular cleaning intervals should be established in the maintenance schedule.
Material Composition
Changes in the chemical composition of the clinker (e.g., variations in iron oxide or alumina content) can slightly alter the dielectric properties. If the kiln feed changes significantly, the moisture sensor may require a recalibration. For comprehensive monitoring of all process variables, including level and flow, engineers often refer to the Main Page of instrumentation providers to select complementary sensors.
Frequently Asked Questions (FAQs)
Q: How often should the moisture sensor be recalibrated?
A: Initially, validation should occur weekly for the first month. Once the system is stable, a monthly or quarterly check against laboratory samples is usually sufficient, unless there is a major change in the raw meal composition.
Q: Can the sensor be used to control the water spray in the cooler automatically?
A: Yes. Once commissioned and validated, the moisture sensor signal is typically used as a feedback variable in a PID loop that regulates the water spray valves. This prevents the clinker from becoming too wet for the cement mills.
Q: What is the impact of clinker grain size on measurement?
A: Microwave sensors are relatively immune to grain size changes. However, NIR sensors can be sensitive to the "shadowing" effect of large clinker nodules. Using a leveling bar to create a smooth surface helps mitigate this.
Q: Is it better to measure moisture on the deep bucket conveyor or the belt conveyor?
A: The belt conveyor is generally preferred because the material is spread thinner and more uniformly, allowing for a more consistent sensor-to-material distance.
Conclusion
A meticulous moisture sensor commissioning checklist cement kiln clinker cooler is the foundation of precise process control in cement manufacturing. By prioritizing correct mechanical placement, rigorous signal integration, and disciplined laboratory validation, plant operators can achieve a reliable moisture measurement. This not only protects downstream equipment like ball mills and conveyors but also contributes significantly to the overall energy efficiency of the plant. For further technical specifications on level and moisture instrumentation, professionals should consult the Main Page for updated product data and application support.
Download Moisture Sensor Commissioning Checklist Cement Kiln Clinker Cooler as a PDF